

Melt Pressure Instability in Extrusion: Causes, Diagnosis, and Solutions
Melt pressure instability in extrusion is caused by one or more of five mechanisms: screw surging from inconsistent feed, screen pack saturation at the filter, thermal variation in the barrel, die restriction changes, or gear pump instability. The most common cause in continuous production is screen pack saturation — which produces progressive ΔP increase and periodic pressure spikes at every screen change. A continuous and self-cleaning screen changer such as the AP Series cleans the screen without stopping the line, greatly reducing the saturation cycle, with minimal pressure disturbance during cleaning.
Why Melt Pressure Stability Determines Product Quality
Melt pressure in an extrusion line is not merely an operating parameter — it is the variable that translates directly into product dimensions. The extruder die converts melt pressure into melt velocity: higher pressure drives more melt through the die gap per unit time, producing thicker sections; lower pressure produces thinner sections. Any variation in melt pressure upstream of the die produces corresponding dimensional variation in the finished product.
Even a few percent of pressure variation upstream of a sheet or film die shows up as gauge variation along the product, and on thin or tightly specified products it can exceed conversion tolerances.
The Five Root Causes of Melt Pressure Instability
Melt pressure instability is not a single phenomenon — it is a symptom with distinct causes that require distinct solutions. Treating instability without identifying the root cause leads to repeated interventions that address symptoms rather than mechanisms. The five causes below cover the full diagnostic range for standard single-screw and twin-screw extrusion lines.
Melt Pressure Instability: Five Causes and Their Solutions
Each cause has a distinct signature in the pressure trace and a specific corrective action. The table below maps cause to symptom pattern to solution.
| Cause | Frequency | Pressure signature | Primary solution |
|---|---|---|---|
| Screen pack saturation | Very common | Progressive rise then spike at screen change; periodic cycle matching change frequency | Continuous and self-cleaning screen changer — greatly reduces the saturation cycle |
| Screw surging | Common | Regular oscillation at a fixed frequency; amplitude proportional to feed inconsistency | Stabilise feed (drying, blending consistency, screw geometry review); gear pump addition |
| Barrel temperature variation | Moderate | Slow drift correlated with ambient temperature or heater band cycling; seasonal pattern | Heater band inspection and replacement; barrel insulation; PID controller calibration |
| Die restriction change | Moderate | Step change in pressure level; often correlated with die cleaning interval or die temperature | Die gap inspection and cleaning; die temperature profile review; die land geometry check |
| Gear pump instability | Less common | High-frequency oscillation (seconds); often with audible signature; independent of screw speed | Gear pump bearing inspection; inlet pressure review; pump sizing verification |
Cause 1: Screen Pack Saturation — the Most Preventable Source of Pressure Instability
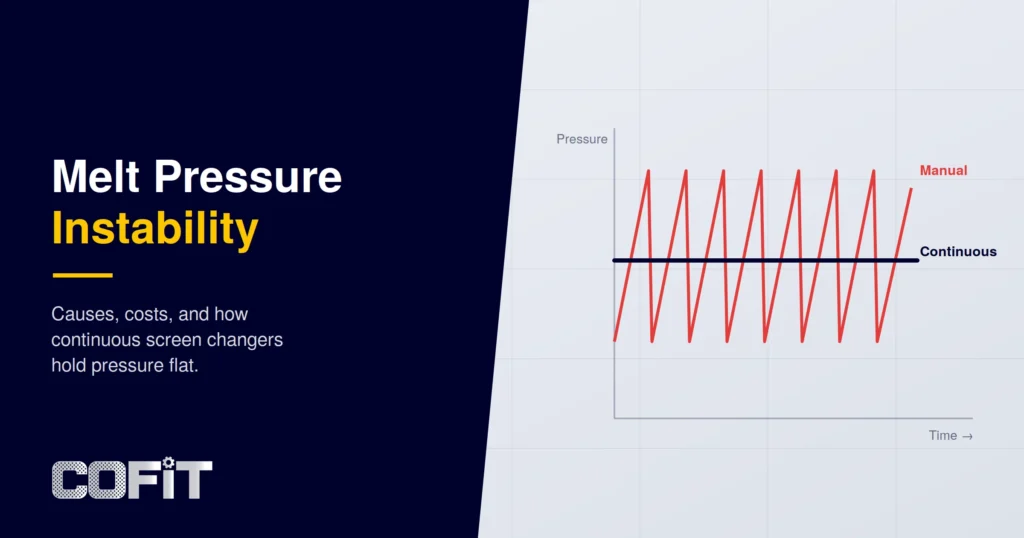
Screen pack saturation is the most common cause of melt pressure instability in continuous production — and one that can be addressed without changing the extruder, the polymer, or the die. As the screen pack accumulates particles, differential pressure (ΔP) across the filter rises progressively. This rising ΔP reduces the effective pressure at the die inlet, reducing melt flow rate and producing thinner product. When the screen is replaced, pressure spikes as the clean screen restores full flow — producing a thicker band.
The resulting pressure variation is not random noise — it is a systematic cycle whose frequency matches the screen change interval. On a line with manual screen changes, the pressure cycle repeats at every change. Every cycle produces a band of gauge variation in the product that is directly traceable to the screen change event.
For how this mechanism specifically affects blown film extrusion, see the full application guide.
Screen pack saturation is one of the main causes of gauge variation in film and sheet extrusion, alongside die temperature non-uniformity and screw instability. Unlike the other two, it is greatly reduced by upgrading to a continuous and self-cleaning screen changer, which cleans the screen before it approaches saturation, with minimal pressure disturbance during cleaning.
For wire, cable and fiber spinning — where saturation at fine mesh makes continuous filtration mandatory — see the wire, cable & fiber extrusion filtration guide.
Diagnosing Screen Pack Saturation vs Other Causes
The diagnostic signature of screen pack saturation is distinctive: a progressive, asymmetric pressure cycle. Pressure rises slowly over the screen life, then drops sharply at the screen change, then recovers with a brief overshoot. This pattern is different from screw surging (symmetric oscillation at a fixed frequency) and barrel temperature variation (slow drift correlated with ambient conditions or heater cycling).
To confirm screen pack saturation as the primary cause, compare the pressure trace with the screen change log. If pressure spikes and drops align precisely with recorded screen change times, the diagnosis is confirmed. If pressure variation continues at the same amplitude after extending screen life or switching to finer mesh, the cause is upstream of the filter.
Cause 2: Screw Surging
Screw surging is periodic oscillation of the melt output from the extruder screw, caused by inconsistent feeding, poor melting efficiency, or screw geometry mismatch with the polymer being processed. It produces a regular pressure oscillation at a fixed frequency that is visible on the upstream pressure transducer and produces corresponding gauge variation in the product.
Common causes include: feed hopper bridging or flow interruption, inconsistent bulk density in regrind or recyclate blends, insufficient drying producing moisture-induced viscosity variation, and screw compression ratio mismatch with a high-viscosity or high-fill compound.
The primary corrective actions are: stabilising the feed (consistent blend preparation, verified drying, hopper level control), reviewing screw geometry for the specific polymer, and — where surging cannot be eliminated at source — adding a melt gear pump downstream of the extruder. A gear pump decouples the output of the extruder screw from the die inlet pressure, absorbing upstream variations and delivering a consistent, pressure-stabilised melt to the die regardless of screw instability.
How Much Is Pressure Instability Costing Your Line?
Screen change frequency is the most common driver of pressure instability — and the most quantifiable. Enter your throughput, stop frequency, and shift schedule to see your monthly output loss.
Causes 3–5: Barrel Temperature, Die Restriction, and Gear Pump
Cause 3: Barrel Temperature Variation
Melt viscosity is strongly temperature-dependent — even a few degrees of barrel temperature variation can change melt viscosity noticeably, especially for polyolefins. Viscosity variation translates directly into melt pressure variation at constant screw speed. Heater band failure or degradation is the most common cause; the pressure trace shows a slow, low-amplitude drift that correlates with heater cycling frequency rather than with screw speed or screen change intervals.
Diagnosis requires cross-referencing the pressure trace with barrel temperature zone logs. If pressure variation correlates with temperature zone cycling in a specific barrel zone, that zone’s heater band and thermocouple should be inspected. Barrel insulation upgrades — particularly on lines in cold environments — reduce temperature cycling amplitude and the associated pressure variation.
Cause 4: Die Restriction Change
The die introduces a defined restriction to melt flow. Any change in die gap, land clearance, or temperature distribution across the die width alters the flow resistance and produces a step change in upstream melt pressure. Die contamination — polymer degradation products accumulating at the die lips or in the manifold — is a common cause on lines running coloured compounds or thermally sensitive polymers. The pressure signature is a step change rather than a cyclic pattern, often correlated with die cleaning intervals or die temperature adjustment events.
Regular die cleaning — scheduled before degradation products reach a critical concentration — prevents contamination-driven restriction changes. Die temperature profile verification after any die gap adjustment confirms that the intended restriction change has been correctly implemented across the full die width.
Cause 5: Gear Pump Instability
Where a melt gear pump is installed between the extruder and die, pump-related instability is characterised by high-frequency pressure oscillation — typically at intervals of seconds rather than minutes — that is independent of screw speed and often accompanied by an audible signature from the pump. Bearing wear, insufficient inlet pressure to the pump (cavitation), or pump sizing mismatch with the throughput range are the primary causes. Gear pump bearing inspection and inlet pressure verification are the first diagnostic steps. A simple test separates the two: hold screw speed constant and vary only the pump speed — if the oscillation frequency follows the pump speed, the pump is the source.
Common Misconceptions About Melt Pressure Instability
“Melt pressure variation is normal in extrusion — a few percent is acceptable and unavoidable.”
Variation is common but not unavoidable. Continuous and self-cleaning filtration and stable feed conditions greatly reduce melt pressure variation on production lines. “Normal” variation in many plants reflects untreated screen pack saturation cycles, not an intrinsic process limit.
“Gauge variation in my film comes from the die — I need to adjust the die lips more frequently.”
If gauge variation follows a periodic pattern aligned with screen change intervals, the root cause is upstream pressure instability — not the die. Adjusting die lips to compensate treats the symptom, not the cause, and introduces a secondary variation source.
“Adding a gear pump will solve all melt pressure instability.”
A gear pump stabilises pressure between the extruder and die — but only if the pressure variation it is correcting is upstream in origin (screw surging). A gear pump does not address screen pack saturation downstream of its position, and cannot compensate for die restriction changes.
“Finer mesh filtration will reduce pressure instability by capturing more particles.”
Finer mesh captures more particles — but also saturates faster, increasing the frequency of the pressure instability cycle. Unless paired with continuous self-cleaning filtration that prevents saturation from occurring, finer mesh makes pressure instability worse, not better.
Reducing Screen Pack Saturation as a Pressure Instability Source
Screen pack saturation is the only one of the five pressure instability causes that is both the most common and the most completely preventable. The solution is not to change screens more frequently — that reduces the amplitude of each pressure event but multiplies the number of events per shift and the associated downtime. The correct solution is to clean the screen without stopping the line, before it saturates.
For sheet extrusion specifically — where gauge variation from pressure instability is a frequent cause of coil rejection — see the sheet extrusion filtration guide →
A continuous self-cleaning screen changer — such as the AP Series — cleans the screen in place before it approaches saturation, keeping the filtration area available and greatly reducing ΔP variation during the production run. The operator uses a key to actuate the flow valves: the resulting backflush of melt cleans the screen, and the cycle completes while melt continues flowing through the parallel filtration area. Pressure disturbance during cleaning is minimal.
Frequently Asked Questions
Melt pressure instability in extrusion is caused by five primary mechanisms: screen pack saturation at the melt filter (most common in continuous production — produces progressive ΔP rise and periodic pressure spikes at screen changes), screw surging from inconsistent feed or screw geometry mismatch, barrel temperature variation from heater band degradation, die restriction changes from contamination accumulation or die gap adjustment, and gear pump instability from bearing wear or cavitation. Each cause has a distinct signature in the pressure trace: screen saturation produces asymmetric periodic cycles; screw surging produces symmetric regular oscillation; barrel temperature variation produces slow correlated drift; die restriction changes produce step changes; gear pump instability produces high-frequency oscillation independent of screw speed.
As a screen pack accumulates particles, differential pressure (ΔP) across the filter rises progressively. Rising ΔP reduces the effective melt pressure at the die inlet, reducing melt flow rate and producing thinner product. When the screen is replaced — whether manually or hydraulically — pressure restores sharply, often with a brief overshoot, producing a thicker band. The result is a systematic pressure cycle whose frequency matches the screen change interval. Continuous and self-cleaning filtration cleans the screen before it saturates and greatly reduces this cycle, with minimal pressure disturbance during cleaning.
Compare your pressure trace with your screen change log. If pressure drops at each recorded screen change and rises progressively between changes, screen pack saturation is confirmed as the primary cause. The pressure signature is asymmetric: a slow rise over the screen life followed by a sharp drop at the change, then a brief recovery overshoot. This pattern is distinct from screw surging (symmetric oscillation at fixed frequency) and barrel temperature variation (slow drift correlated with ambient or heater cycling). If pressure variation continues at similar amplitude after extending screen life, the cause is upstream of the filter — likely screw or barrel.
No. A gear pump is installed between the extruder and the die to decouple extruder output instability (screw surging) from die inlet pressure. It stabilises pressure variation originating upstream of the pump — but screen pack saturation occurs downstream of the extruder and either downstream of the pump (if the screen changer is after the pump) or upstream of the pump discharge (if the screen changer is between extruder and pump). In either configuration, the gear pump does not address ΔP variations caused by screen saturation. The correct solution for screen saturation-driven pressure instability is continuous self-cleaning filtration that prevents saturation from occurring.
Acceptable variation depends on the product: thin films, high-clarity film, optical sheet and barrier coextrusion need tighter control than standard sheet. A continuous and self-cleaning screen changer such as the AP Series cleans the screen without stopping the line, with minimal pressure disturbance during cleaning. For applications requiring even tighter control, continuous filtration combined with a melt gear pump is the standard process architecture.
Tackle Screen Pack Saturation at the Source
If your pressure variation pattern aligns with your screen change log, continuous self-cleaning filtration is the solution — not more frequent changes, not die adjustments, not screw modifications. Calculate your current downtime cost first, then speak with a Cofit engineer about the right filtration specification for your line.
Cofit deals with research, engineering, manufacture and distribution of screen changers that keep the line running, including for post-consumer and post-industrial recycled materials.
Contact us to upgrade your extrusion system or ask us for more information about any product or service.